NFE25511 French Serrated Spring Washers

Product Overview


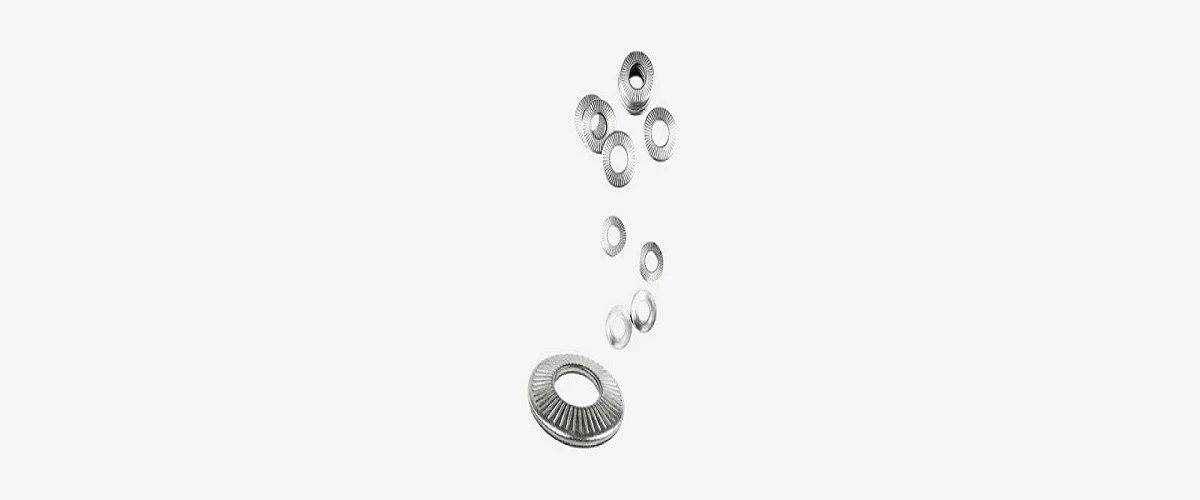
NFE25511 French serrated spring washers provide mechanical locking for high-vibration bolted joints through controlled elastic preload and radial serrations. Conforming to the French standard NF E 25-511, these washers feature asymmetrical or dual-sided serration teeth that bite into both the bolt head/nut bearing surface and the mating substrate. When tightened, the conical body flattens to maintain constant tension while the serrations mechanically interlock against rotational self-loosening induced by cyclic shock and vibration.


Product Types & Configurations


AZ Type (Single-Sided Serration):

Features teeth on one side to bite into the bolt head while the smooth underside glides against the component surface, preventing damage to soft substrates.


SKR Type (Dual-Sided Serration):

Incorporates serrations on both top and bottom faces, establishing a positive mechanical grip on both the fastener head and the clamped material.


Dimensions:

Standard metric sizes ranging from M3 through M30, engineered for standard clearance holes per ISO 273.


Key Features

Bite-Type Locking Mechanism:

Radial teeth penetrate oxide layers and coatings, creating a direct metal-to-metal frictional barrier against vibrational rotation.

Elastic Recovery:

Conical spring geometry acts as an energy accumulator, compensating for thermal expansion, initial embedment, and joint relaxation.

Controlled Hardness Gradient:

Core hardness maintained between 420 HV and 520 HV ensures teeth retain sharp geometric profiles without undergoing brittle fracture under heavy clamp loads.

Reusability Factor:

Serration design minimizes thread and joint distortion, permitting disassembly and re-tightening within specified maintenance cycles.


Materials & Surface Options
 
productcate-1200-500
 

Spring Steel (60Si2Mn / C75S):

High tensile strength base material quenched and tempered to 420-520 HV.


Stainless Steel (AISI 304 / A2, AISI 316 / A4):

Selected for corrosion-resistant environments and chemical processing equipment.

productcate-1200-500
 

Zinc Flake Coating:

Applied via dip-spin coating to achieve 720 to 1,000 hours of neutral salt spray resistance (ASTM B117) with zero risk of hydrogen embrittlement.


Electro-Zinc Plating:

Clear or yellow passivation (8-12 micrometers) with mandatory post-plate baking at 190 deg C for 4 hours to eliminate residual hydrogen stress in high-carbon steel variants.

productcate-1200-500


Applications
01.

Automotive Powertrains:

Securing transmission housings, exhaust flanges, and subframe mountings subjected to continuous engine harmonics.

02.

Railway Track Infrastructure:

Fastening rail clips, fishplates, and signaling equipment exposed to high-frequency dynamic axle loads.

03.

Wind Energy Turbines:

Locking internal tower flange connections, nacelle brackets, and yaw gear drive assemblies.

04.

Heavy Construction Equipment:

Hydraulic excavator arm joints, track roller frames, and vibratory compactor assemblies.


Manufacturing & Quality Control


Blanking & Stamping:


High-speed mechanical stamping presses (25T to 200T) utilizing progressive tungsten carbide dies to maintain burr-free inner and outer diameters.

01

Forming & Serration Broaching:

Precision cold-forming stations that press radial teeth with exact depth, angle, and symmetry tolerances.

02

Heat Treatment:


Continuous atmosphere belt furnaces (Endothermic gas with automated carbon potential control) for uniform austenitizing, oil quenching, and tempering.

03

Dimensional Inspection:


Automated optical sorting machines checking thickness, inner/outer diameter, and tooth profile at 1,200 parts per minute.

04

Metallurgical Testing:


In-house laboratory verifying micro-hardness via Vickers indenters, decarburization depth limits, and hydrogen embrittlement relief baking compliance.

05


Customization & OEM

Custom Geometry:

Non-standard inner/outer diameters, altered tooth angles, and heavy-duty thickness profiles manufactured to customer engineering drawings.

Traceability & Marking:

Lot number laser-etched on packaging batches; Material Test Reports (MTR) provided per EN 10204 3.1.

Packaging Solutions:

VCI (Volatile Corrosion Inhibitor) anti-rust poly bags, bulk industrial cartons, or automated assembly line blister packs tailored to Kanban and 5S bin-stocking protocols.


FAQ


Q: What is the primary mechanical difference between NFE25511 washers and standard DIN 127 split lock washers?

A: DIN 127 split washers flatten under load and often lose spring tension due to plastic deformation under dynamic vibration. NFE25511 serrated conical washers utilize combined spring elasticity and physical serration bite to resist rotational loosening without relying solely on friction under the nut.

Q: How do you prevent hydrogen embrittlement during the plating of high-carbon spring steel?

A: Parts plated with electrolytic zinc undergo mandatory baking within 2 hours of electro-deposition at 190 deg C for a minimum of 4 hours. Alternatively, zinc flake coatings are applied via a non-electrolytic thermal cure process, eliminating hydrogen introduction entirely.

Q: Can NFE25511 washers be reused after routine equipment maintenance?

A: Yes, provided the serration teeth and conical spring deflection remain within tolerance. Technicians must inspect the bite marks and free height during disassembly; discard washers exhibiting flattened teeth or severe mechanical scoring.

Q: What is the recommended tightening torque adjustment when switching from flat washers to serrated lock washers?

A: Standard torque charts calculated for lubricated plain fasteners generally apply, but the increased friction coefficient of biting serrations may require a minor torque calibration (+5% to +10%) to achieve equivalent clamp load. Consult the joint calculation sheet (VDI 2230) for specific applications.

Q: What minimum surface hardness is required for the mating component to prevent washer embedment?

A: The mating flange or joint surface must possess a hardness level below that of the washer (420-520 HV), but sufficiently high (typically > 200 HB / 20 HRC for structural steel) to prevent excessive sinkage or bearing surface deformation under the serration teeth.

Q: What documentation is supplied with commercial shipments for quality verification?

A: Every shipment includes an EN 10204 3.1 Inspection Certificate detailing chemical composition of the melt, raw material tensile strength, heat treatment hardness logs, and salt spray test compliance records.

As one of the most professional nfe25511 french serrated spring washers manufacturers and suppliers in China, we're featured by quality products and good service. Please rest assured to buy customized nfe25511 french serrated spring washers made in China here from our factory. For more information, contact us now.

NFE25511 French br Serrated Spring Washers, nfe25511 french serrated spring washers

(0/10)

clearall